The world of welding is vast and complex, with numerous electrode types available for different applications. Among these, the 7018 welding rod stands out as a versatile and widely-used option, particularly in industries demanding high-strength, low-alloy steel welds. Understanding the different types of 7018 welding rod – variations in chemical composition, coating types, and diameter – is crucial for achieving optimal weld quality, efficiency, and cost-effectiveness.
Globally, the demand for reliable welding solutions continues to grow, driven by infrastructure development, manufacturing, and energy sectors. According to the World Bank, global infrastructure investment is projected to reach trillions of dollars in the coming decades, significantly increasing the need for skilled welders and high-quality welding consumables like the 7018 rod. The proper selection of the right 7018 welding rod ensures structural integrity and longevity in critical applications.
The increasing scrutiny on weld quality and safety, especially in industries like oil and gas, aerospace, and shipbuilding, underscores the importance of expertise in different types of 7018 welding rod. Choosing the appropriate rod type minimizes defects, reduces rework, and ultimately lowers project costs. This specialized knowledge is no longer a niche skill but a fundamental requirement for many professional welders.
The Significance of Understanding Different Types of 7018 Welding Rod
The 7018 welding rod is renowned for its low-hydrogen characteristics and excellent mechanical properties, making it ideal for welding critical structures. However, not all 7018 rods are created equal. Variations in manufacturing processes, alloy compositions, and coating formulations result in distinct rod types tailored for specific applications. Recognizing these differences is paramount to achieving high-quality welds and ensuring long-term structural integrity. different types of 7018 welding rod can greatly influence the result.
Understanding the nuances of different types of 7018 welding rod empowers welders to select the optimal rod for the material being welded, the welding position, and the desired weld characteristics. This targeted approach minimizes defects like porosity and cracking, reduces the need for costly rework, and improves overall welding efficiency.
Defining Different Types of 7018 Welding Rod
The designation “7018” itself is a coding system established by the American Welding Society (AWS). The ‘70’ indicates a minimum tensile strength of 70,000 psi, while the ‘18’ signifies the welding position and type of coating. Specifically, ‘1’ means it can be used in all positions, and ‘8’ denotes a low-hydrogen, iron powder coating. However, within this standard, manufacturers produce variations in the chemical composition and manufacturing process, resulting in different types of 7018 welding rods.
These variations often cater to specific application requirements. Some 7018 rods are optimized for deep penetration welds, while others excel in producing smooth, aesthetically pleasing beads. Still others are formulated to offer improved weldability in challenging conditions, such as welding over rusty or contaminated surfaces. Choosing the right rod necessitates understanding these subtle but impactful differences.
The core of a 7018 rod is a low-carbon steel wire. The coating, a complex mixture of iron powder, flux materials, and binders, plays a vital role in shielding the weld pool from atmospheric contamination, adding alloying elements, and stabilizing the arc. Subtle changes in the coating composition directly impact the rod's performance characteristics.
Core Characteristics of 7018 Welding Rods
The defining characteristic of 7018 rods is their low-hydrogen content. The heavy coating, rich in iron powder, creates a shielding gas when heated, protecting the molten weld metal from absorbing moisture from the atmosphere. This is crucial because hydrogen can cause cracking and reduce the ductility of the weld. Proper storage – keeping the rods in a moisture-controlled environment – is critical to maintaining this low-hydrogen characteristic.
7018 rods are known for their excellent mechanical properties, including high tensile strength, good ductility, and resistance to cracking. This makes them suitable for welding high-strength low-alloy steels and critical structural components. The weld metal exhibits good toughness and can withstand significant stress and fatigue.
These rods typically require a DC+ (direct current electrode positive) polarity for optimal performance. The arc produced is stable and easy to control, even in out-of-position welding. However, maintaining a proper arc length and travel speed is vital to prevent defects and achieve a sound weld.
Key Factors Influencing 7018 Welding Rod Performance
Several factors impact the performance of different types of 7018 welding rod. Chemical composition, particularly the levels of manganese, silicon, and carbon, influences the weld metal's strength, ductility, and weldability. Different manufacturers may adjust these levels to tailor the rod for specific applications.
The coating type is another crucial factor. The ratio of iron powder to flux materials affects the arc stability, penetration, and slag removal. Some coatings contain alloying elements like nickel or chromium to enhance the weld metal's corrosion resistance or strength.
Comparative Performance of different types of 7018 welding rod
Global Applications and Use Cases of 7018 Welding Rod
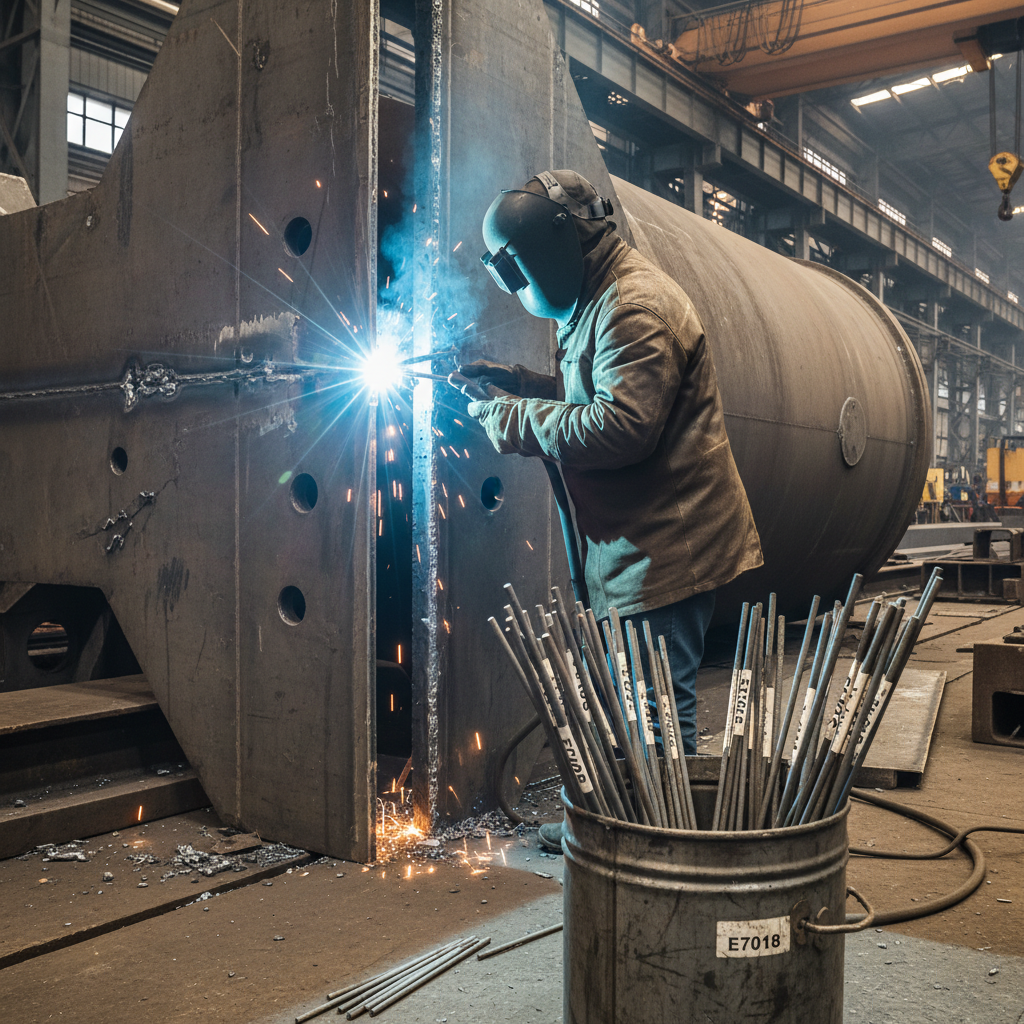
7018 welding rods find extensive use in a multitude of industries worldwide. In the construction sector, they are crucial for welding structural steel in bridges, buildings, and other infrastructure projects. Their reliable performance and high strength make them ideal for these demanding applications.
The oil and gas industry relies heavily on 7018 rods for pipeline construction and repair, as well as for welding pressure vessels and offshore platforms. The low-hydrogen characteristics are essential to prevent cracking in these critical components. Similarly, the shipbuilding industry utilizes these rods extensively for hull fabrication and repair.
Advantages and Long-Term Value of Using 7018 Welding Rods
The primary advantage of 7018 rods lies in their ability to produce high-quality, low-hydrogen welds with excellent mechanical properties. This translates to improved structural integrity, increased durability, and reduced risk of failure. These rods are also relatively easy to use, even for less experienced welders, thanks to their stable arc and forgiving characteristics.
From a long-term perspective, selecting the appropriate type of 7018 rod contributes to cost savings by minimizing rework and reducing maintenance requirements. High-quality welds last longer and require fewer repairs, resulting in lower lifecycle costs. The reliability and durability of these welds also enhance safety and reduce the potential for catastrophic failures.
Future Trends and Innovations in 7018 Welding Rod Technology
Ongoing research and development efforts are focused on improving the performance and sustainability of 7018 welding rods. New coating formulations are being explored to enhance arc stability, reduce spatter, and improve weld metal properties. Automation and robotic welding are also driving demand for rods with consistent and predictable performance.
There's a growing trend towards "greener" welding solutions, with manufacturers seeking to reduce the environmental impact of their products. This includes developing coatings with lower levels of volatile organic compounds (VOCs) and exploring the use of more sustainable raw materials. Digital technologies, such as weld monitoring systems, are also being integrated to optimize welding parameters and ensure weld quality.
Furthermore, advancements in artificial intelligence and machine learning are being leveraged to predict weld defects and optimize welding processes. This could lead to the development of “smart” 7018 rods that automatically adjust their performance based on real-time welding conditions.
A Summary of Key Considerations for Choosing the Right 7018 Welding Rod
| Material Compatibility |
Welding Position |
Joint Design |
Desired Weld Properties |
| Carbon Steel (Low Alloy) |
All Positions |
Butt, Lap, Fillet |
High Tensile Strength, Ductility |
| Mild Steel |
Flat, Horizontal |
T-Joint, Corner Joint |
Good Penetration, Smooth Beads |
| High-Strength Low-Alloy Steel |
Vertical Up, Overhead |
Pipe Welds, Pressure Vessels |
Low Hydrogen, Crack Resistance |
| Corrosion-Resistant Steel |
All Positions (with proper preheating) |
Flange Connections, Tank Welds |
Corrosion Resistance, Weld Integrity |
| Dirty or Rusty Surfaces |
Flat, Horizontal |
Repair Welds, Maintenance |
Forgiving Arc, Good Wetting Action |
| Thin Sheet Metal |
Flat, Horizontal |
Sheet Metal Fabrication |
Low Heat Input, Minimal Distortion |
FAQS
Proper storage is paramount for maintaining the low-hydrogen properties of 7018 rods. Ideally, rods should be stored in a sealed container in a dry environment. If the container has been opened or the rods have been exposed to humidity, it’s recommended to bake them at a low temperature (around 200-300°F) for a specified period – typically one hour per inch of rod diameter – to remove absorbed moisture. Always consult the manufacturer's recommendations for specific baking instructions.
7018 welding rods generally require DC+ (Direct Current Electrode Positive) polarity for optimal performance. This polarity provides deeper penetration and a more stable arc. While some specialized 7018 rods might be designed for AC welding, DC+ is the standard recommendation for most applications. Using the incorrect polarity can lead to poor weld quality, instability, and difficulty maintaining a consistent arc.
Visually inspect the rods for cracks, broken coatings, or excessive rust. If the coating is significantly damaged, the rod’s low-hydrogen properties may be compromised. Expired rods may also exhibit a chalky or brittle coating. If you suspect the rods are damaged or expired, it’s best to discard them and use a fresh batch to ensure weld quality. Check the manufacturing date on the packaging as a reference.
The '70' in 7018 indicates a minimum tensile strength of 70,000 psi (pounds per square inch). However, the actual tensile strength achieved in a weld can vary depending on factors such as the base metal, welding parameters, and heat treatment. Properly executed 7018 welds generally exhibit excellent tensile strength, making them suitable for high-stress applications.
While it's technically possible to weld cast iron with 7018 rods, it's generally not recommended. Cast iron has different metallurgical properties than steel, and 7018 rods are designed primarily for steel welding. Specialized cast iron electrodes are preferable for achieving strong, durable welds on cast iron materials. Using 7018 rods on cast iron can lead to cracking and poor weld quality.
“Low-hydrogen” refers to the minimized amount of hydrogen present in the weld metal. Hydrogen can readily absorb into molten weld metal from atmospheric moisture. The coating on 7018 rods shields the weld pool from the atmosphere, preventing hydrogen absorption. Excess hydrogen can cause hydrogen-induced cracking, a serious weld defect. Therefore, maintaining the low-hydrogen properties through proper storage and welding techniques is critical for ensuring weld integrity.
Conclusion
Understanding the nuances of different types of 7018 welding rod is essential for achieving high-quality, reliable welds in a wide range of applications. From selecting the appropriate rod for the material being welded to implementing proper storage and welding techniques, attention to detail is paramount. The versatility and proven performance of 7018 rods continue to make them a cornerstone of the welding industry.
As technology advances, we can expect to see further innovations in 7018 welding rod formulations and welding processes. Embracing these advancements, alongside a commitment to best practices, will be crucial for welders and fabricators seeking to maximize efficiency, minimize defects, and ensure the long-term integrity of their work. For a comprehensive selection of high-quality 7018 welding rods, visit our website: www.jinlongweldingelectrode.com