Look, I've been running around construction sites for, what, fifteen years now? You see a lot of things. A lot. And lately? Everyone's screaming about lightweight, high-strength materials. Carbon fiber this, graphene that… It’s a phase, honestly. Good stuff, don’t get me wrong, but often overhyped. People forget, a good, solid weld is still king. You need a reliable welding rod manufacturer, that’s where it starts and ends, really.
I swear, engineers design things on computers, no real-world feel. They’ll spec out some fancy alloy, then expect the welders to make magic happen. Have you noticed how many designs are a nightmare to actually fit? Too tight a radius, impossible angles… They don’t think about the guy actually holding the torch. To be honest, it drives me crazy. And the tolerances! They’ll ask for a .01-inch gap, and then wonder why the weld’s cracking.
It’s all about the details, right? Seems simple, but it's not. And it all comes back to sourcing. You need a welding rod manufacturer who understands the metal they're working with, and the conditions you’re working in. Because some rods are just… brittle. Snap easily. Then you’re wasting time, money, and patience.
The Current Trends in Welding Materials
Honestly, the biggest trend I'm seeing is the push for automation. Robotic welding, that sort of thing. It's good for repetitive tasks, sure. But try getting a robot to weld a pipe in a tight space, or adapt to a slightly warped piece of steel? Forget about it. That’s when you need a skilled welder and a good welding rod manufacturer that delivers consistent quality.
And everyone’s chasing higher tensile strengths, lighter weights. Titanium, stainless steel alloys…they look good on paper. But those materials can be a pain to work with. They require specific shielding gases, precise welding techniques. A cheap rod isn’t going to cut it with that stuff, believe me.
Common Design Pitfalls in Welding Applications
I encountered this at a factory in Shanghai last time. They designed a support beam with a ridiculously small weld prep area. The engineer swore it would hold. It didn't. Bent like a paperclip. Strangely, he was surprised. It’s always the surprises. They don’t think about heat-affected zones, stress concentrations… it's all about getting it to look good in the CAD software.
Another common mistake? Ignoring corrosion. You weld two different metals together, and you create a galvanic cell. Then throw it into a salty environment… you’re asking for trouble. We need more corrosion-resistant alloys, or at least proper coatings. And a good welding rod manufacturer can advise on compatible filler metals, which is huge.
And the worst? Designs that require welding in awkward positions. Overhead, vertical… it increases the risk of porosity, undercut, all sorts of defects. Sometimes, a slight redesign can make all the difference. But nobody wants to pay for that, do they?
Materials We Use: From Steel to Specialized Alloys
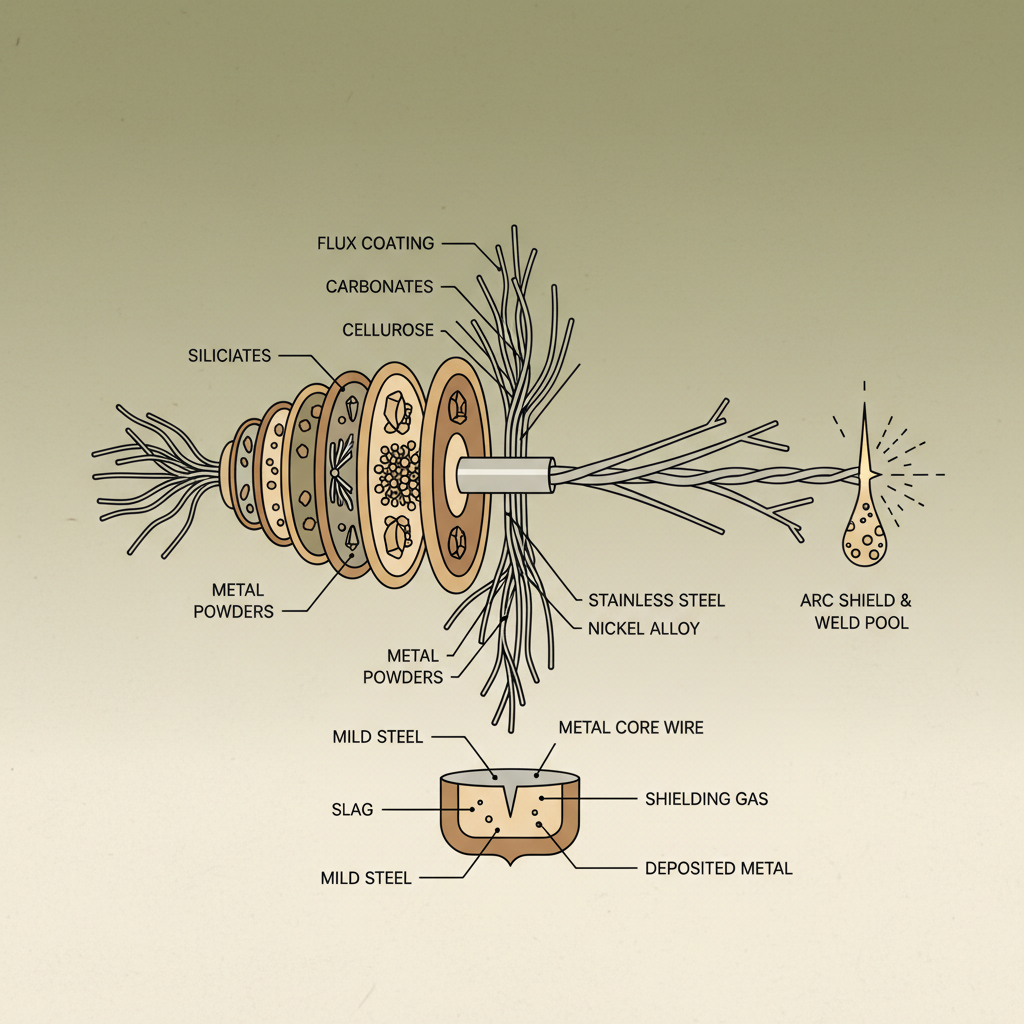
We mostly work with mild steel, obviously. The workhorse of the industry. You can smell it, you can feel the weight. It's solid. Then you've got low-alloy steels, for higher strength. Stainless steel is common, especially for food processing and marine applications. It feels…slick, different. You need to be careful with stainless, it can overheat quickly.
And then you get into the more exotic stuff. Inconel, Hastelloy... these are expensive. They’re used in high-temperature, corrosive environments. The rods for these are different too – a little more finicky. They sometimes have a coating, and you have to be careful not to damage it before welding. Honestly, I prefer sticking with what I know, but sometimes you don’t have a choice.
The key is knowing your material, and choosing the right rod. A good rod smells… right. Seriously. You can tell if it’s been stored properly, if it’s absorbed moisture. Moisture is the enemy. Ruins the weld. Always store them in a dry place, and bake them if you're unsure.
Real-World Testing & Quality Control
Forget the lab tests. Those are useful, sure, but they don’t tell the whole story. We test welds by bending them, hammering them, sometimes even dropping things on them. It sounds barbaric, but it works. If it cracks, it fails. Simple as that.
We also do visual inspections, of course. Look for porosity, undercut, incomplete fusion. A good welder can spot a bad weld a mile away. And we use dye penetrant testing for critical welds. It finds hairline cracks that you wouldn't see otherwise. I saw it used a lot when I was working on a pipeline.
Welding Rod Performance: Key Metrics
How Workers Actually Use Welding Rods
You know, what the spec sheet says and what happens on the ground are often two different things. I've seen guys use the wrong amperage, the wrong polarity, and still get a decent weld. It's all about feel. Experience. They compensate. They adjust. And sometimes, they just brute-force it.
And they don’t always follow the procedures. I’m not saying it's right, but it happens. Especially when they're under pressure to meet a deadline. They'll take shortcuts. That's why a good welding rod manufacturer has a reputation for being forgiving, you know? Something that can handle a little abuse.
Advantages & Disadvantages: A Pragmatic View
Look, a good welding rod lets you get the job done quickly and reliably. It minimizes defects, reduces rework, and saves money in the long run. That’s the advantage. But they’re not perfect. Some rods create a lot of spatter, which is a pain to clean up. Some generate a lot of fumes, which is bad for your health. And some are just plain expensive.
Anyway, I think the biggest disadvantage is inconsistency. You can buy a batch of rods from the same welding rod manufacturer, and they can still vary slightly in composition or diameter. It’s frustrating. That's why building a relationship with a supplier you trust is so important.
Customization and Specific Applications
We had a client, a small boss in Shenzhen making smart home devices, last month. Insisted on changing the connector on their product to , even though it meant having to weld a tiny connector onto a very small circuit board. The result? A massive increase in defects. He wouldn't listen. Said it was “future-proofing”. Later… forget it, I won't mention it.
But customization is possible. You can get rods with different alloying elements, different coatings, different diameters. We once had a job where we needed a rod with a specific manganese content to weld a particular type of high-strength steel. The welding rod manufacturer was able to make it happen, but it wasn't cheap.
And then there's the application. Submerged arc welding requires different rods than TIG welding. Pipe welding requires different rods than structural steel welding. It’s all about matching the rod to the process and the material.
A Quick Reference Guide for Common Welding Rod Characteristics
| Rod Type |
Typical Applications |
Key Advantages |
Potential Drawbacks |
| E6010 |
General purpose, dirty/rusty steel |
Deep penetration, easy arc starting |
Produces a lot of spatter, requires a clean base metal |
| E7018 |
Structural steel, high-strength applications |
Low spatter, good ductility, smooth arc |
Requires a clean base metal, slower deposition rate |
| E308L-16 |
Stainless steel welding |
Excellent corrosion resistance, good weldability |
Expensive, can be sensitive to overheating |
| E7014 |
Sheet metal, light fabrication |
Easy to use, good for beginners, flat & horizontal positions |
Not suitable for dirty or rusty steel |
| E11018 |
High-strength low alloy steel |
High tensile strength, good toughness |
Requires preheating and post-weld heat treatment |
| E6013 |
All positions, general purpose |
Easy arc starting, forgiving |
Not ideal for high strength applications |
FAQS
E6010 rods are great for digging deep into dirty or rusty metal, perfect for initial root passes. They're easy to start an arc with but produce a lot of spatter. E7018 rods, on the other hand, are better for multi-pass welds and offer lower spatter and better ductility, but require a cleaner base metal. Choosing the right one really depends on the job and the steel condition. A good welding rod manufacturer will have both.
Moisture is the enemy! Always store your rods in a sealed container or cabinet. If you suspect they’ve absorbed moisture, you need to bake them to drive it out. Follow the manufacturer's instructions for baking temperature and time – usually around 250-300°F for an hour. Don't skip this step, or you'll end up with porous, weak welds.
Amperage depends on the rod diameter, the type of metal you're welding, and the joint configuration. The rod packaging will usually have a recommended amperage range. Start in the middle of the range and adjust as needed. Too low, and you won’t get enough penetration. Too high, and you’ll burn through the metal. It's best to practice and find what works best for your setup.
Look for inconsistencies in the coating, excessive rust, or damaged packaging. A good rod should have a smooth, even coating and feel solid. If it feels brittle or crumbly, it’s probably not worth using. Also, a reputable welding rod manufacturer will have consistent quality control.
Porosity can be caused by several things: moisture in the rod or base metal, contamination, incorrect gas shielding, or insufficient welding current. Proper preparation is key – clean the metal thoroughly, use dry rods, and ensure adequate shielding gas coverage. Sometimes it’s as simple as adjusting the amperage.
Not all rods are created equal! Some are specifically designed for flat and horizontal positions, while others are suitable for all positions, including vertical and overhead. Check the rod’s classification to see which positions it’s approved for. Using the wrong rod in the wrong position can lead to weak, unreliable welds.
Conclusion
So, there you have it. Welding isn’t just about joining pieces of metal together. It's about understanding the materials, the processes, and the real-world conditions. Choosing the right welding rod manufacturer, and using their products correctly, is crucial for building safe, durable, and reliable structures. It's the foundation of everything we do.
Ultimately, whether this thing works or not, the worker will know the moment he tightens the screw. If the metal holds, you've done your job. And that's what really matters. If you’re looking for quality welding rods and a partner you can trust, check out www.jinlongweldingelectrode.com. They know their stuff.