

Expert Guide to the selection of electrode in welding for Success

Expert Guide to the selection of electrode in welding for Success
Jun . 26, 2026 14:50
Mastering the Selection of Electrode in Welding for Industrial Success
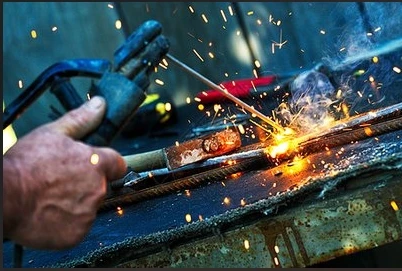
Achieving a high-quality weld starts long before the arc is struck; it begins with the precise selection of electrode in welding. Whether you are working on heavy structural steel or delicate thin-plate components, the choice of electrode determines the mechanical strength, appearance, and longevity of the joint. Using the wrong filler material can lead to porosity, cracking, or insufficient penetration, compromising the safety of the entire structure. In this guide, we will explore the critical factors involved in choosing the right welding consumables to ensure professional-grade results in the manufacturing sector.

Understanding Base Metal Compatibility
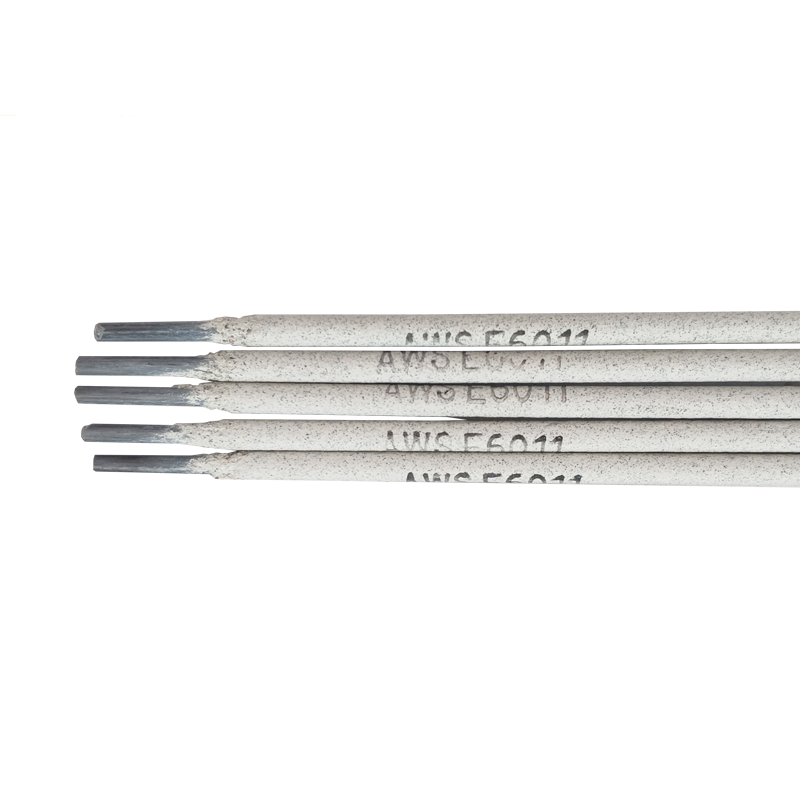
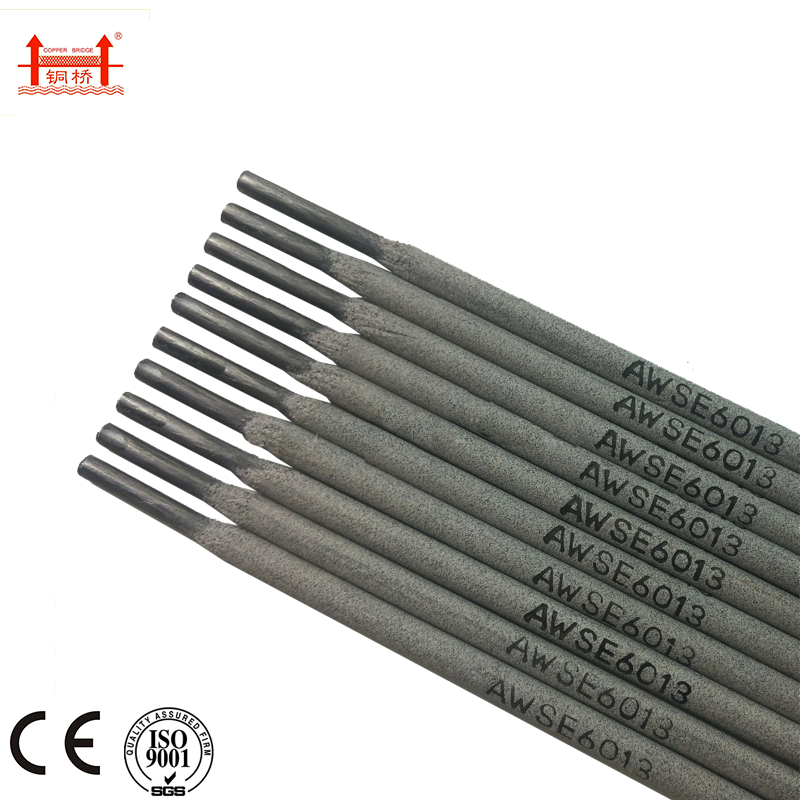
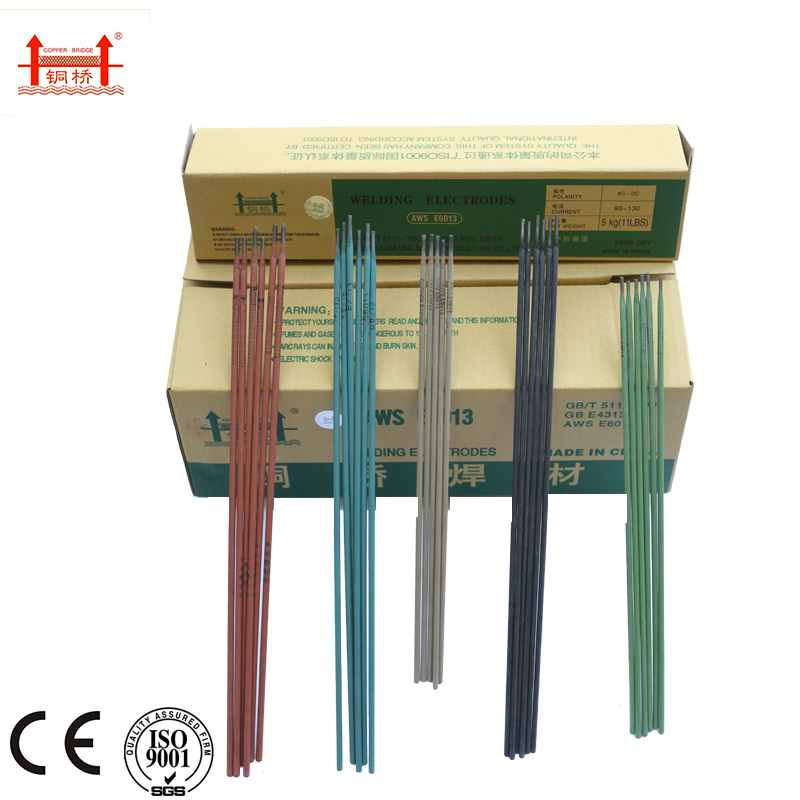
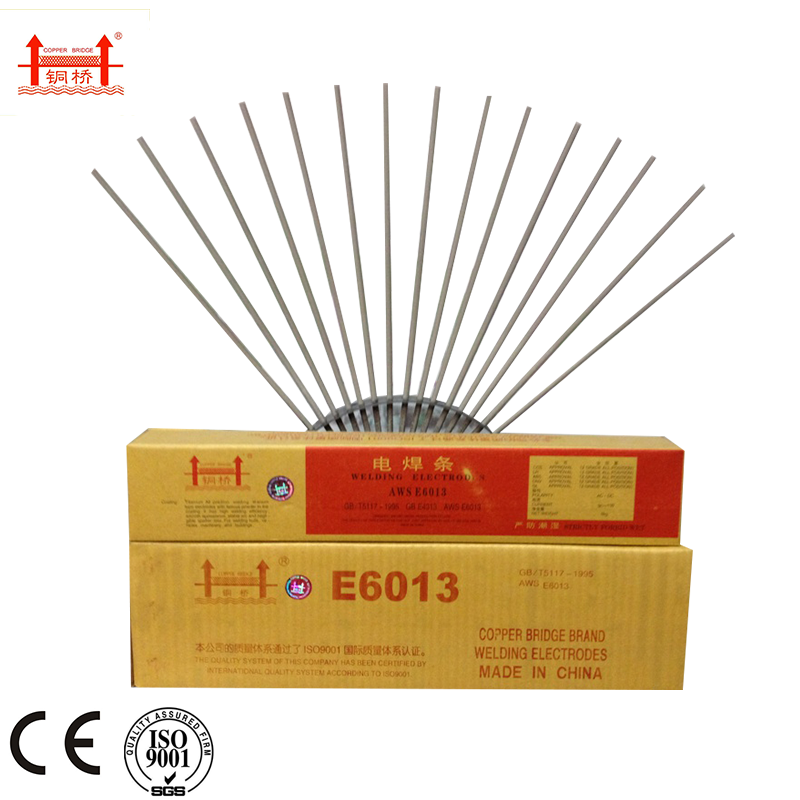
The primary rule in the selection of electrode in welding is matching the electrode's chemical composition to the base metal. For low-carbon steel structures, electrodes like the E6013 are industry standards due to their versatility. When the deposited metal matches the base metal in terms of tensile strength and carbon content, the risk of thermal cracking is minimized. Professionals must consider the chemical composition, specifically the levels of Manganese and Silicon, to ensure the weld pool flows correctly and bonds securely with the parent material.
Comparing Coating Types for Different Finishes
Coating types play a pivotal role in determining the arc stability and the final appearance of the weld. Titania-type coatings are highly regarded for their ease of use and smooth welding passes, making them ideal for thin plate steel and short discontinuous welds. On the other hand, cellulosic or basic coatings are preferred for deep penetration in heavy industrial pipes. Choosing between AC and DC current capability also depends on your power source, but most modern titania electrodes support both, offering greater flexibility on the job site.
Pro Tip: For those requiring a smooth, aesthetic finish with minimal spatter, the E6013 titania-coated electrode is the optimal choice for low carbon steel applications.
Technical Specifications for Selection of Electrode in Welding
To make an informed selection of electrode in welding, one must analyze the technical data sheet. The following table provides a detailed breakdown of the CB-J421 (E6013) model, showcasing its mechanical properties and chemical composition, which are essential for quality control in metal fabrication.
Optimizing Electrode Diameter and Current
Once the material is matched, the next step in the selection of electrode in welding is choosing the correct diameter. A diameter that is too large for thin plates can lead to burn-through, while one that is too small for thick sections will result in poor fusion. Common diameters such as 3/32, 1/8, and 5/32 must be paired with the correct amperage to maintain a stable arc and a consistent bead width.

Storage and Maintenance Requirements
Even the perfect selection of electrode in welding can be ruined by poor storage. Moisture is the enemy of welding rods, often leading to hydrogen-induced cracking. While titania electrodes generally do not require baking before first use, any rod exposed to high humidity should be baked at 150℃-170℃ for 0.5 to 1 hour. This process removes absorbed moisture and ensures the integrity of the chemical coating, maintaining the promised mechanical properties of the deposited metal.
Application Scenarios in Metal Fabrication
In the metal products manufacturing industry, versatility is key. The use of E6013 electrodes is widespread because they are suitable for a vast array of applications, from simple household repairs to complex low-carbon steel structures. Their ability to provide a smooth welding pass makes them the go-to choice for thin plates where aesthetics are as important as strength. By adhering to standardized selection criteria, manufacturers can ensure consistent quality across all production batches.
Conclusion: The Impact of Correct Electrode Selection
The selection of electrode in welding is a technical decision that directly impacts the structural integrity and cost-efficiency of any project. By matching the electrode to the base metal, selecting the appropriate coating, and maintaining strict storage protocols, you can avoid costly rework and ensure a professional finish. For high-performance low-carbon steel welding, trust in certified, high-quality consumables to bridge the gap between a basic weld and an engineering masterpiece.
Frequently Asked Questions (FAQs)
Why is the selection of electrode in welding so critical for thin plates?
For thin plates, the primary risk is burn-through and excessive distortion. A carefully selected electrode, such as the titania-type E6013, provides a stable arc and a smoother weld pool that can be controlled more easily. This ensures that the heat input is sufficient for fusion but not so high that it melts through the base metal. Using a rod with a diameter that matches the plate thickness is essential to maintain this balance and achieve a clean, professional finish without the need for extensive grinding.
Do I always need to bake my welding electrodes?
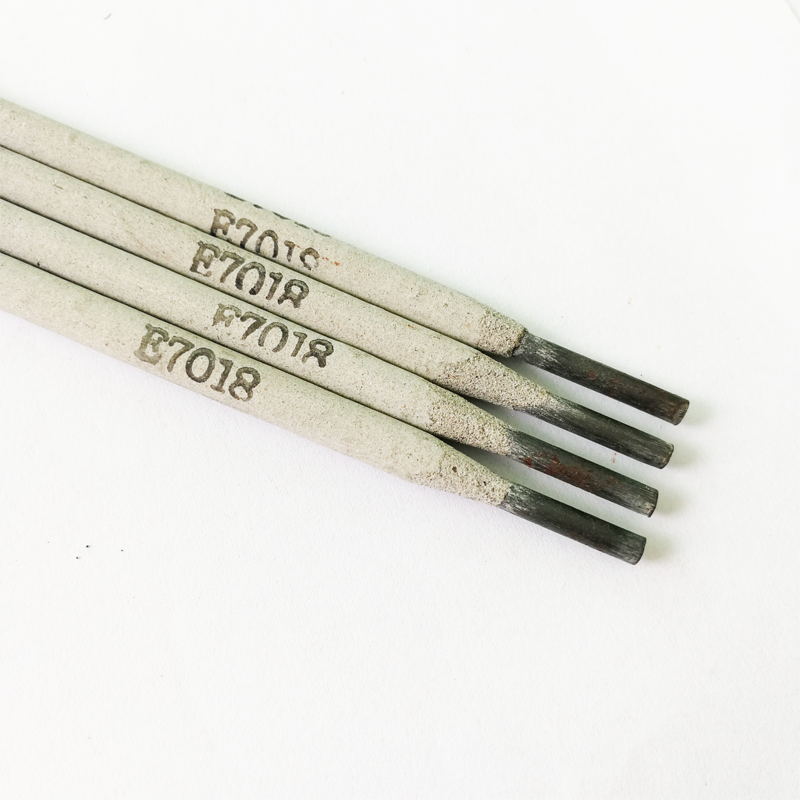
Not all electrodes require baking. For example, titania-type rods generally do not need pre-welding baking if they have been stored in a dry environment. However, low-hydrogen electrodes (like E7018) almost always require baking to maintain their properties. If your electrodes have been exposed to moisture or stored in a humid warehouse, baking them at 150℃-170℃ for about an hour is recommended. This prevents the formation of hydrogen pores in the weld, which can significantly weaken the joint and lead to premature failure.
What is the difference between AC and DC electrodes?
The difference lies in the chemistry of the coating and the core wire, which determines how the electrode reacts to the electrical polarity. AC (Alternating Current) electrodes are versatile and can be used with basic buzz-box welders. DC (Direct Current) electrodes allow for more control over heat distribution—DC+ (Reverse Polarity) typically provides deeper penetration, while DC- (Straight Polarity) is better for thinner materials. Many modern electrodes, including the ones found at Jinlong Welding Electrode, are designed to work efficiently with both current types.
How do I determine the correct diameter for my project?
The diameter is typically chosen based on the thickness of the base metal and the joint design. A general rule of thumb is that the electrode diameter should be proportional to the thickness of the material being welded. For very thin sheets, 3/32" is often preferred to keep heat input low. For medium-thickness structural steel, 1/8" is the standard. For thick plates or filling large gaps, 5/32" or larger is used to increase deposition rates. Always refer to the welding procedure specification (WPS) for precise requirements to ensure the weld meets safety standards.


Related Video

Related News
2026-07-01 09:32:39
Comprehensive Guide to Selection of Types of Welding Rods PDF
Selecting the correct filler metal is the cornerstone of any successful welding project. Whether you are working on heavy-duty carbon steel pipelines or intricate structural components, understanding the various types of welding rods pdf resources is essential for ensuring weld integrity and structural safety. The choice of electrode affects not only the strength of the joint but also the ease of penetration and the final appearance of the bead. In this comprehensive guide, we will explore the technical specifications of high-performance rods, such as the CB-J425, to help you optimize your manufacturing process.
2026-06-29 16:50:39
Comprehensive Guide to Types of Welding Rods and Uses PDF
Comprehensive Guide to Types of Welding Rods and Uses PDF Selecting the correct filler metal is the most critical step in ensuring the structural integrity and corrosion resistance of any welded joint. For professionals seeking a detailed types of welding rods and uses pdf , understanding the distinction between various alloys is essential. Whether you are working with chromium stainless steel for power plants or chromium-nickel variations for medical machinery, the choice of electrode directly impacts the welds longevity. In this guide, we analyze the technical specifications and industrial applications of high-performance welding electrodes to help you achieve precision and durability in every bead.
2026-06-27 15:42:52
Guide to Types of Welding Electrodes and Their Uses PDF Manual
Understanding Types of Welding Electrodes and Their Uses PDF Guide Selecting the correct filler metal is critical for the structural integrity and longevity of any welded joint. Whether you are working in power plants, chemical processing, or petroleum equipment, knowing the types of welding electrodes and their uses pdf documentation provides the necessary technical foundation to avoid common failures like cracking or corrosion. Chromium stainless steel and chromium-nickel alloys offer specialized resistance to oxidizing acids and high temperatures, but they require precise handling. This guide explores the technical specifications and application methods for high-performance electrodes to ensure professional-grade welding results.
2026-06-26 14:50:28
Expert Guide to the selection of electrode in welding for Success
Mastering the Selection of Electrode in Welding for Industrial Success Achieving a high-quality weld starts long before the arc is struck; it begins with the precise selection of electrode in welding . Whether you are working on heavy structural steel or delicate thin-plate components, the choice of electrode determines the mechanical strength, appearance, and longevity of the joint. Using the wrong filler material can lead to porosity, cracking, or insufficient penetration, compromising the safety of the entire structure. In this guide, we will explore the critical factors involved in choosing the right welding consumables to ensure professional-grade results in the manufacturing sector.
2026-06-25 16:48:22
Professional Guide on how to choose welding rod size for Steel
Mastering the Art of Welding: How to Choose Welding Rod Size Selecting the correct filler metal is one of the most critical decisions a welder makes to ensure the structural integrity and aesthetic quality of a joint. Understanding how to choose welding rod size can mean the difference between a professional-grade weld and a failure-prone joint. Whether you are working with mild steel, carbon steel, or low alloy steel, the diameter of your rod directly impacts heat input, penetration depth, and the overall efficiency of the process. In this guide, we will explore the technical factors that influence sizing
2026-06-23 05:10:11
Mastering Stainless Steel Welding with e308l 16 amps Guide
Mastering the E308L 16 Amps Setting for Perfect Stainless Steel Welding Achieving a high-quality weld on stainless steel requires a precise balance of material science and machine calibration. When utilizing e308l 16 amps , the welder must consider the relationship between current, heat input, and penetration. E308L is a low-carbon variant of the 308 stainless steel electrode, designed specifically to prevent carbide precipitation and ensure maximum corrosion resistance. In this guide, we will explore how managing the amperagespecifically focusing on the 16-amp range for thin gaugescan drastically improve the structural integrity and aesthetic finish of your industrial projects.
2026-06-21 05:05:43
Ultimate Guide to Choosing the Right 304 tig rod for Welding
In the world of precision welding, selecting the correct filler metal is the difference between a structural failure and a flawless finish. The 304 tig rod is one of the most widely used consumables in the industry, prized for its exceptional corrosion resistance and versatility. Whether you are working on food processing equipment, chemical containers, or architectural accents, understanding the nuances of ER308L the standard filler for 304 stainless is essential. This guide provides a professional deep dive into the specifications, applications, and best practices for using these rods to ensure high-quality, durable welds.
2026-06-20 05:10:16
Precision Welding Guide for SS Welding Rod 2.5 mm Electrode
Mastering Precision Welding with SS Welding Rod 2.5 mm In the world of high-precision fabrication, the choice of consumables can make or break the structural integrity of a project. The ss welding rod 2.5 mm is a cornerstone for professionals seeking a perfect balance between penetration and control. Whether you are working on intricate food-grade piping or heavy-duty industrial supports, selecting a rod with the correct diameter is essential for minimizing distortion and ensuring a clean, slag-free finish. This guide will explore the technical nuances, application methods, and comparative advantages of using a 2.5 mm stainless steel welding electrode to achieve industrial-grade results.

 English
 Arabic
 Bengali
 China
 French
 German
 Hausa
 Indonesian
 Italian
 Japanese
 Javanese
 Malay
 Persian
 Portuguese
 Punjabi
 Russian
 Spanish
 Swahili
 Telugu
 Vietnamese