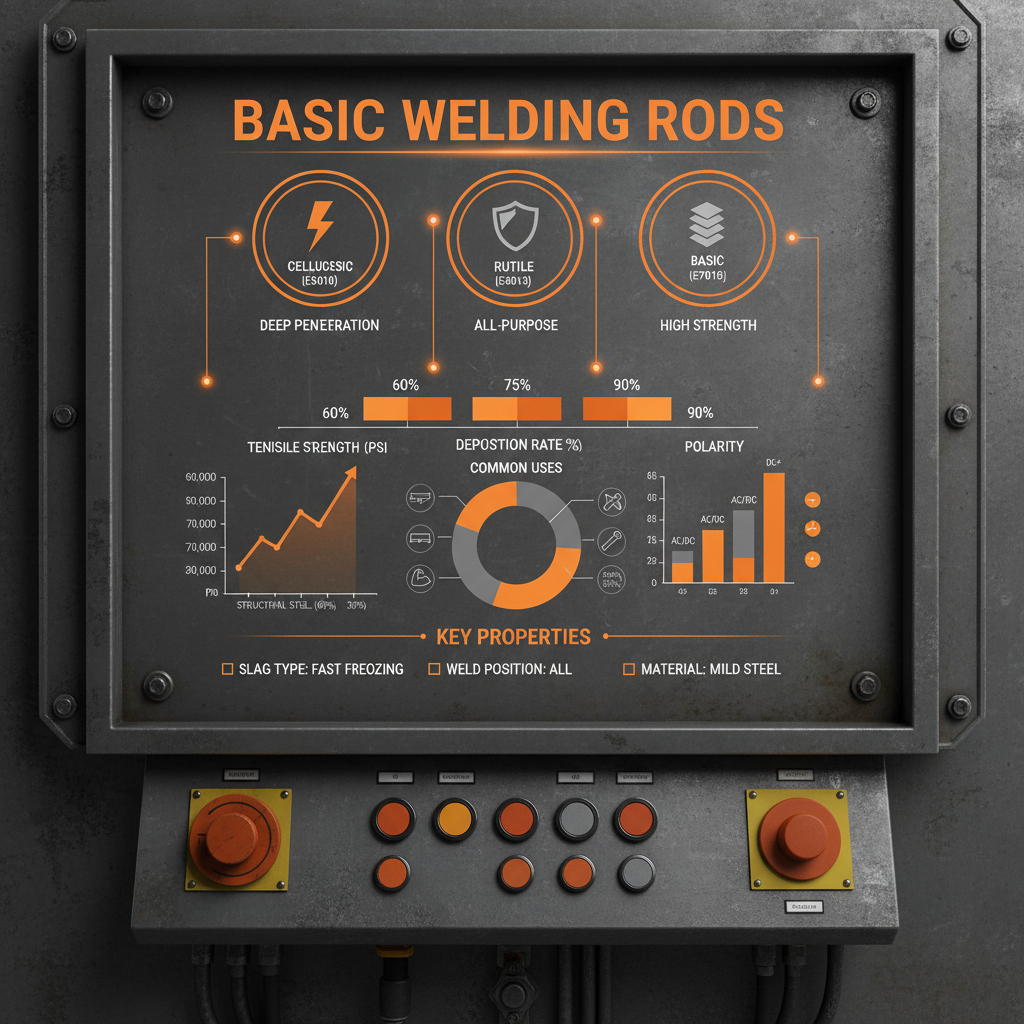
Selecting the right welding consumable is a critical decision that directly impacts the structural integrity, longevity, and safety of any metal fabrication project. Whether you are working on heavy industrial machinery or precision chemical equipment, understanding the relationship between base metal chemistry and filler material is the only way to ensure a defect-free weld. For many professionals, learning how to choose electrode for welding is the difference between a high-performance joint and a costly failure.
Across the global manufacturing sector, the demand for specialized alloys has increased as industries push the boundaries of heat and corrosion resistance. From power plants to petroleum refineries, the choice of electrode must align with the specific mechanical properties required, such as tensile strength and elongation. Miscalculating the electrode type often leads to issues like hydrogen cracking, porosity, or insufficient penetration, which can compromise entire infrastructure projects.
In this comprehensive guide, we will explore the technical nuances of selecting the correct rods, focusing specifically on the complexities of stainless steel and carbon steel applications. By mastering the criteria of how to choose electrode for welding, you can optimize your workflow, reduce waste, and ensure that your finished products meet rigorous international standards such as AWS specifications.
Material Compatibility and Base Metal Analysis
The first step in determining the correct filler is a deep analysis of the base metal. For instance, chromium stainless steel provides excellent corrosion resistance against oxidizing and organic acids, as well as high heat and wear resistance, making it indispensable for power plants and chemical equipment. However, these materials often exhibit poor weldability, requiring a precise match between the electrode and the base metal to avoid structural failure.
When dealing with specific grades like CR-13 stainless steel, the risk of cracking increases significantly due to high hardness after welding. In such cases, the user must decide between using a matching chromium stainless steel electrode (such as G202 or G207) with strict preheating, or opting for a chromium-nickel stainless steel electrode (A107 or A207) if post-weld heat treatment is not feasible.
The Impact of Coating Types on Weld Quality
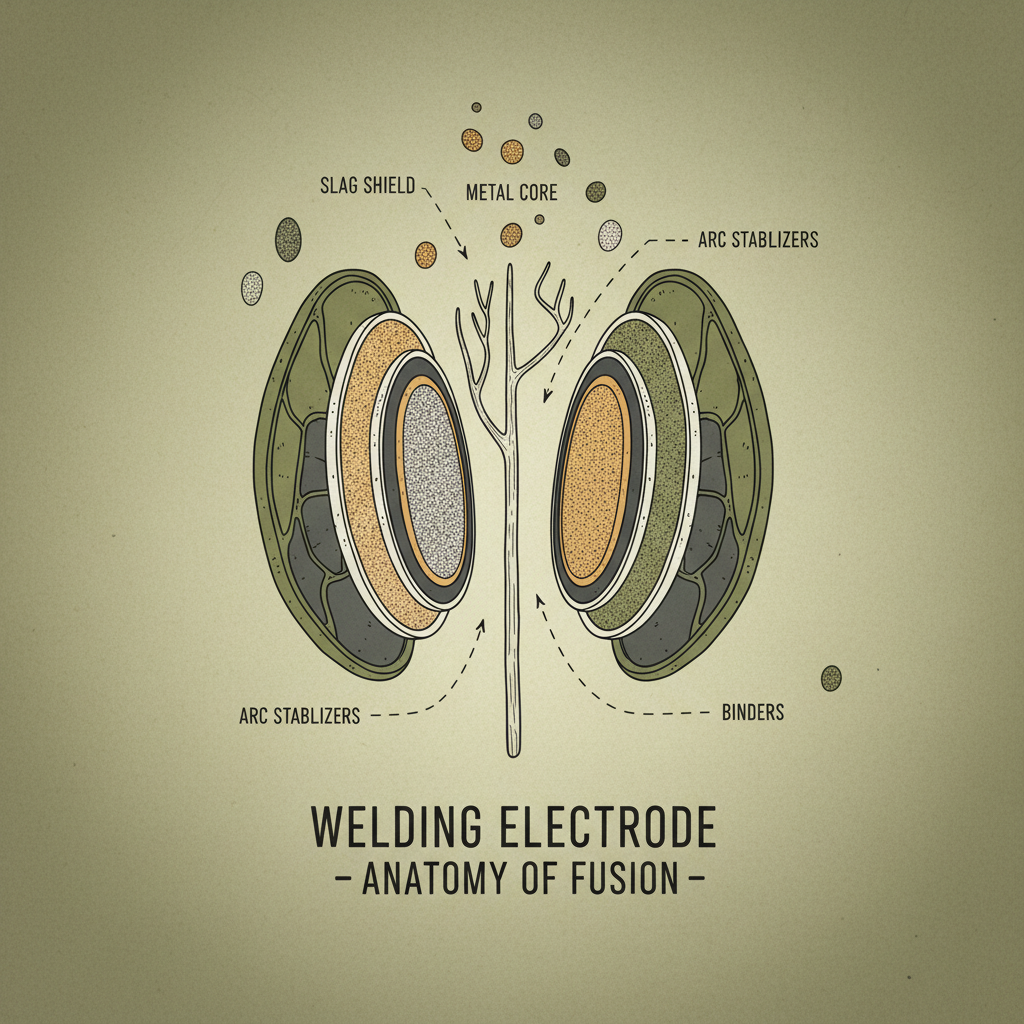
The coating of a welding electrode determines the arc stability, slag formation, and the chemical composition of the weld pool. For chromium-nickel stainless steel, coatings typically fall into two categories: titanium-calcium type and low hydrogen type. Understanding these differences is essential for any technician wondering how to choose electrode for welding based on their power source.
Titanium-calcium coatings are versatile, as they can be used with both AC and DC power supplies. However, AC welding often results in shallow penetration and a tendency for the weld to redden. To achieve a deeper, more stable weld with better penetration, DC power is strongly recommended for these specific coatings.
Low hydrogen coatings are designed to minimize the introduction of hydrogen into the weld metal, which is crucial for preventing cold cracking in high-strength alloys. By selecting the correct coating, welders can control the mechanical properties of the deposited metal, ensuring the joint is as strong as the surrounding base material.
Managing Thermal Stress and Heat Treatment
Thermal management is a non-negotiable aspect of how to choose electrode for welding when working with high-alloy steels. For example, Chromium 17 stainless steel incorporates stability elements like Ti, Nb, and Mo to improve weldability and corrosion resistance. Even so, these materials require specific thermal protocols to maintain their integrity.
If a matching chromium stainless steel electrode (G302, G307) is utilized, a preheating temperature above 200 °C is required, followed by tempering around 800 °C. If the project constraints prevent post-weld heat treatment, the only safe alternative is to switch to a chromium-nickel stainless steel electrode, such as A107 or A207, which manages thermal stress more effectively.
Furthermore, controlling the heat input during the welding process prevents intergranular corrosion. This is achieved by keeping the welding current approximately 20% lower than what would be used for carbon steel electrodes, maintaining a short arc, and ensuring quick cooling between layers to produce a narrow, high-quality bead.
Positional Welding and Diameter Selection
The physical dimensions and the operational position of the weld are key factors in deciding the rod diameter. Generally, electrodes with smaller diameters are suited for all-position welding, providing the flexibility needed for complex joints. Conversely, larger diameters are restricted to flat and fillet welding positions where gravity allows for better puddle control.
When considering how to choose electrode for welding for specific tasks, the diameter must be balanced against the thickness of the base metal to ensure full penetration without burning through the workpiece.
Effectiveness of Electrode Selection by Application
Corrosion Resistance in Harsh Environments
CR-NI stainless steel electrodes are specifically engineered for environments where oxidation and corrosion are primary threats. These electrodes are widely utilized in the manufacturing of medical machinery, petroleum equipment, and fertilizer plants, where the materials are constantly exposed to aggressive chemicals.
When solving the puzzle of how to choose electrode for welding for these industries, the focus shifts to the chemical composition of the deposited metal. For example, the CB-A102 (AWS E308-16) is ideal for welding corrosion-resistant structures like 0Cr19Ni9 and 0Cr19Ni11Ti stainless steel, operating effectively in temperatures below 300 °C.
Storage and Maintenance of Electrodes
Even the most technically correct electrode will fail if it is not stored and maintained properly. Moisture absorption in the coating can lead to hydrogen-induced cracking and porosity in the weld bead. To prevent this, electrodes must be kept dry and subjected to specific baking cycles before use.
Titanium-calcium type electrodes should be dried at 150 °C for one hour, while low hydrogen types require a higher temperature of 200 °C to 250 °C for one hour. It is critical to avoid repeated drying, as this can cause the coating to crack or peel off, rendering the electrode unusable.
Additionally, keeping the electrode free from oil and dirt is paramount. Contaminants on the coating can increase the carbon content of the weld, which directly degrades the corrosion resistance and overall quality of the joint, undermining the effort put into how to choose electrode for welding.
Technical Specification Comparison for Selection
For a truly scientific approach to selection, one must look at the chemical composition and mechanical properties of the deposited metal. The ratio of Carbon (C), Manganese (Mn), Silicon (Si), Nickel (Ni), and Chromium (Cr) determines how the weld will behave under stress and exposure to corrosive agents.
For instance, a deposit with a Chromium content of 18.0-21.0% and Nickel content of 9.0-11.0% ensures that the weld metal matches the corrosion resistance of the base stainless steel. This level of detail is the core of professional-grade selection processes.
Mechanical properties, such as the tensile strength (Rm) and elongation (A%), provide the final validation. A tensile strength of ≥550 Mpa and elongation of ≥35% ensure that the weld can withstand operational loads without brittle failure.
Technical Parameters of Stainless Steel Electrodes for Material Selection
|
Electrode Model / AWS
|
Coating Type
|
Recommended Current
|
Primary Application
|
| CB-A102 (E308-16) |
Lime-titania |
DC |
0Cr19Ni9 Stainless Steel |
| G202 / G207 |
Chromium Based |
DC/AC |
CR-13 Stainless Steel |
| G302 / G307 |
Chromium Based |
DC/AC |
Chromium 17 Steel |
| A107 / A207 |
Cr-Ni Based |
DC |
Non-Heat Treated Alloys |
| Low Hydrogen Type |
Low-H |
DC |
High Strength Structures |
| Titanium-Calcium |
Ti-Ca |
AC/DC |
General Purpose Stainless |
FAQS
For CR-13 stainless steel, you have two primary options depending on your ability to perform heat treatment. If you can preheat the metal above 300°C and cool it around 700°C post-welding, use a matching chromium stainless steel electrode like G202 or G207. If post-weld heat treatment is impossible, you must select a chromium-nickel stainless steel electrode (A107 or A207) to prevent cracking due to high hardness.
Titanium-Calcium coatings are versatile and compatible with both AC and DC power, though DC is preferred for better penetration. Low Hydrogen coatings are specifically designed to reduce hydrogen pickup in the weld, which is critical for preventing cold cracking in high-stress applications. They also require higher drying temperatures (200-250°C) compared to Titanium-Calcium types (150°C).
The current for stainless steel electrodes is typically kept about 20% lower than that of carbon steel to prevent intergranular corrosion. Excessive heat can cause chromium carbides to precipitate at the grain boundaries, leaving the area depleted of chromium and vulnerable to corrosion. Using a lower current and ensuring quick cooling between layers helps maintain the material's protective properties.
Electrodes must be kept dry to avoid porosity. Titanium-calcium types should be dried at 150°C for 1 hour, and low hydrogen types at 200-250°C for 1 hour. Crucially, do not repeat the drying process, as this can cause the coating to crack and peel. Additionally, ensure the rods are free from oil or dirt to prevent carbon contamination of the weld pool.
No. Generally, only electrodes with smaller diameters are suitable for all-position welding. Larger diameter electrodes are typically reserved for flat and fillet welding because they deposit more metal and require a position where the molten pool is easier to control via gravity. Always check the manufacturer's specifications for the specific diameter and position ratings.
CR-NI (Chromium-Nickel) electrodes offer superior corrosion and oxidation resistance, making them the gold standard for chemical, fertilizer, and petroleum industry equipment, as well as medical machinery. They are designed to maintain their integrity in highly aggressive environments where standard carbon steel or low-alloy electrodes would fail rapidly.
Conclusion
Mastering how to choose electrode for welding requires a holistic understanding of material science, thermal dynamics, and precise application techniques. By matching the electrode chemistry to the base metal—whether it be the specific requirements of CR-13 or the high corrosion resistance of CR-NI—and adhering to strict drying and current protocols, welders can ensure structural joints that are both durable and safe. The integration of correct coating types and diameter selection further optimizes the process for different welding positions and power sources.
As industrial requirements move toward more extreme environments and tighter tolerances, the reliance on high-performance consumables like AWS E308-16 and specialized chromium alloys will only grow. We recommend that fabricators always prioritize technical data sheets over guesswork and maintain rigorous storage standards to prevent material degradation. For those seeking the highest quality welding consumables and professional guidance, visit our website: www.jinlongweldingelectrode.com.