

How to Choose Copper Coated Mild Steel Wire for MIG Welding

How to Choose Copper Coated Mild Steel Wire for MIG Welding
Nov . 04, 2026 02:40
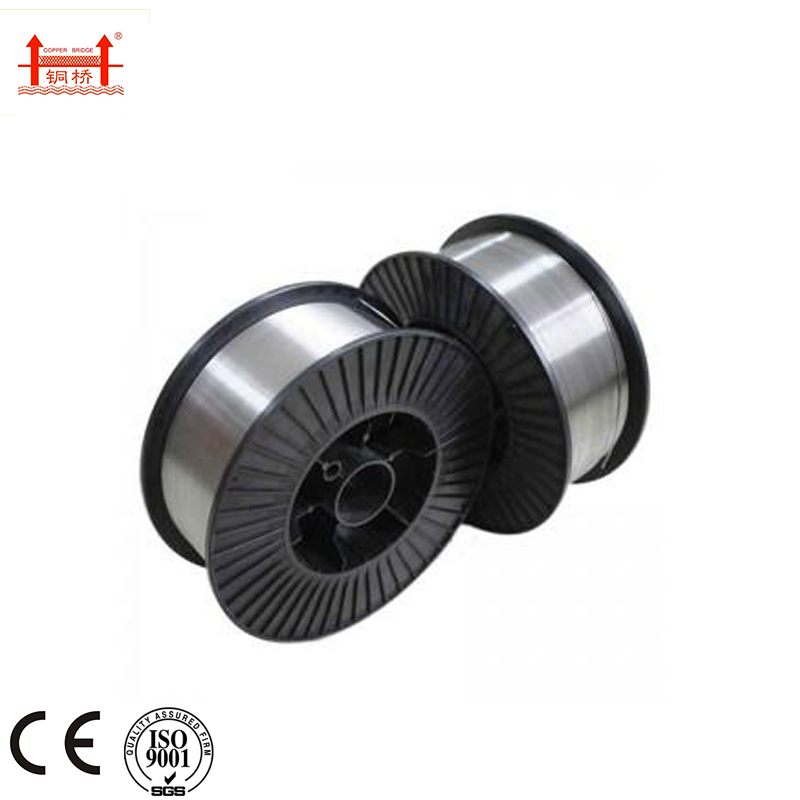
Copper coated mild steel wire should match the base metal, wire diameter, welding process, and equipment setup. Our AWS ER70S-6 wire is intended for mild steel, carbon steel, and low alloy steel, with diameters from 0.6 mm to 1.2 mm. Its copper coating supports electrical conductivity, while low spatter, steady arc behavior, and feedability suit repeated welding work. Use the checklist below to specify the correct wire for your operation.

Base-metal compatibility: mild steel, carbon steel, or low alloy steel
Wire diameter: AWS ER70S-6 sizes from 0.6 mm to 1.2 mm
Welding setup: process, current arrangement, feeder, and equipment compatibility
Feeding and cleanup needs: feedability, steady arc behavior, low spatter, and welding-run length
Copper coated mild steel wire is selected by the material being joined, the wire diameter, and the welding setup. Our AWS ER70S-6 welding wire suits mild steel, carbon steel, and low alloy steel. It is available in diameters from 0.6 mm to 1.2 mm for welding work that needs a copper-coated wire with electrical conductivity, low spatter, and good feedability.
The product fits professional welders, fabrication shops, and DIY users. A buyer preparing a MIG work cell should specify the wire grade, diameter, and required quantity together. The product name alone does not identify the size needed by the feeder.
Match the base metal first
AWS ER70S-6 is intended for mild steel, carbon steel, and low alloy steel. Start with the grade and thickness of the material in the joint, then select the wire that matches the welding procedure for that job.
A fabrication shop joining mild steel sections can use the stated material range as the first application check. If the same workshop handles carbon steel components, the wire remains relevant when the joint and procedure call for AWS ER70S-6. Low alloy steel work also falls within the stated material range, but the material grade and joint details should be included in the purchasing request.
Send the base-metal grade and joint details with your inquiry. This keeps the wire choice tied to the actual work instead of a broad label such as copper coated mild steel wire.
Select the diameter for the equipment
The AWS ER70S-6 range is 0.6 mm to 1.2 mm. Diameter affects the fit between the wire, contact parts, feeder, and welding procedure, so each work cell should have its required size identified before ordering.
A shop with lighter fabrication tasks may use a smaller size within the range, while a different joint and equipment arrangement may call for a larger size. The correct selection depends on the joint, material thickness, feeder setup, and procedure. Do not group several sizes under one purchasing line if they will be installed in different machines.
For example, a workshop with two MIG stations should list the required diameter for each station. Labeling the spool by work cell helps the operator load the intended wire and reduces the chance of mixing sizes during production.
Check the welding process and current
Use AWS ER70S-6 when the welding operation is set up for this wire and its stated application. The product is identified for MIG welding, TIG welding, and Shielded Metal Arc Welding. The process selected for the job must match the equipment, current arrangement, wire diameter, and workplace procedure.
For a MIG operation, specify the current arrangement and feeder setup with the order details. The copper coating promotes electrical conductivity, while good feedability and a steady arc support controlled wire movement through the equipment. These features matter during repeated joints, where feeding interruptions can slow the operator and interrupt the welding run.
The process should be decided before the spool is assigned to a machine. Include the process, current type, base metal, and diameter in the same inquiry so we can discuss the suitable configuration.
Consider spatter and long welding runs
Low spatter can reduce the cleaning required after welding. Good feedability and a steady arc are useful when the work includes long runs and repeated joints.
Picture a fabrication operator joining a series of mild steel sections. The operator needs the wire to move consistently through the feeder while maintaining the selected welding procedure. A buyer handling this type of work should compare the required diameter and quantity for each work cell, then plan the spool request around the number of joints and the expected welding runs.
These characteristics support selection decisions, but they do not replace the settings and safety practices required for the selected equipment and process.
Who should choose this wire
Choose our Plastic Metal Spool Gas Protection Copper Coated product when your job requires AWS ER70S-6 wire for mild steel, carbon steel, or low alloy steel and the required diameter is between 0.6 mm and 1.2 mm. It suits professional welding work, fabrication shops, and DIY projects that use the stated material range and compatible welding setup.
The product is a practical fit when you need:
- Copper coating to promote electrical conductivity.
- A wire diameter from 0.6 mm to 1.2 mm.
- Use with mild steel, carbon steel, or low alloy steel.
- Low spatter for less post-weld cleaning.
- Good feedability and a steady arc for repeated or long welding runs.
What to send when ordering
Provide these details for each required spool or work cell:
- Base-metal grade and joint details.
- Welding process and current arrangement.
- Required AWS ER70S-6 diameter, from 0.6 mm to 1.2 mm.
- Feeder and equipment setup.
- Joint type and whether the work includes long runs.
- Required spool or package quantity.
Send the material grade, joint drawing, wire diameter, process, and quantity with your quotation request so we can review the application fit and prepare the appropriate product details.

About the author
The company
Dingzhou Jinlong Metal Production Co., Ltd.
Dingzhou Jinlong Metal Production Co., Ltd. is located in the industrial zone of Dingzhou city, Hebei province, China. We are professional factory of welding electrodes(welding rods), welding wire, welding blend powder, welding material, machete and nails, with powerful strengthen and advanced technology and the rights of self-supporting export. We introduced the international advanced level of electrodes production line and complete test equipment, our annual output is 50000 tons.…
About Us ↗Visit company website ↗Have a project in mind?
Send us the application, sizes and quantity and we will come back with a matching configuration.


Related Video

Related News
2026-11-04 02:40:06
How to Choose Copper Coated Mild Steel Wire for MIG Welding
Choose copper coated mild steel wire by base metal, AWS ER70S-6 diameter, welding setup, feedability, and spatter requirements.
2026-10-30 11:59:25
Is Flux Core Better Than MIG? FAQ for E71T-GS Welding Wire
Is flux core better than MIG? Compare documented E71T-GS self-shielded flux core wire with gas-shielded MIG solid wire by application, polarity, diameters, shielding, and mechanical data.
2026-10-27 23:20:02
Gas Shielded Welding Wire Selection Guide: Application Fit and Specification Checks
Compare CB-ER50-3 through CB-ER60-G gas shielded welding wire grades by tensile class, plate thickness, and industry application. Specification tables and a pre-order checklist included.
2026-10-27 23:18:34
Choosing Copper Bridge Welding Electrodes 6013 6011 7018: Application Fit and Specification Checks
Compare application fit and specifications for Copper Bridge Welding Electrodes 6013 6011 7018. Learn which diameter suits your plate thickness, position requirements, and material grade before ordering from Dingzhou Jinlong Metal Production Co., Ltd.
2026-10-22 23:27:30
Stainless Steel Electrode Price Comparisons: Choosing E316L-16 by Application Fit and Specification Checks
Compare stainless steel electrode price quotes like-for-like: check the published E316L-16 classification, 2.5 to 5.0 mm diameters, AC/DC use, chemistry and strength, and when E347-16 fits instead.
2026-07-01 09:32:39
Comprehensive Guide to Selection of Types of Welding Rods PDF
Selecting the correct filler metal is the cornerstone of any successful welding project. Whether you are working on heavy-duty carbon steel pipelines or intricate structural components, understanding the various types of welding rods pdf resources is essential for ensuring weld integrity and structural safety. The choice of electrode affects not only the strength of the joint but also the ease of penetration and the final appearance of the bead. In this comprehensive guide, we will explore the technical specifications of high-performance rods, such as the CB-J425, to help you optimize your manufacturing process.
2026-06-29 16:50:39
Comprehensive Guide to Types of Welding Rods and Uses PDF
Comprehensive Guide to Types of Welding Rods and Uses PDF Selecting the correct filler metal is the most critical step in ensuring the structural integrity and corrosion resistance of any welded joint. For professionals seeking a detailed types of welding rods and uses pdf , understanding the distinction between various alloys is essential. Whether you are working with chromium stainless steel for power plants or chromium-nickel variations for medical machinery, the choice of electrode directly impacts the welds longevity. In this guide, we analyze the technical specifications and industrial applications of high-performance welding electrodes to help you achieve precision and durability in every bead.
2026-06-27 15:42:52
Guide to Types of Welding Electrodes and Their Uses PDF Manual
Understanding Types of Welding Electrodes and Their Uses PDF Guide Selecting the correct filler metal is critical for the structural integrity and longevity of any welded joint. Whether you are working in power plants, chemical processing, or petroleum equipment, knowing the types of welding electrodes and their uses pdf documentation provides the necessary technical foundation to avoid common failures like cracking or corrosion. Chromium stainless steel and chromium-nickel alloys offer specialized resistance to oxidizing acids and high temperatures, but they require precise handling. This guide explores the technical specifications and application methods for high-performance electrodes to ensure professional-grade welding results.

 English
 Arabic
 Bengali
 China
 French
 German
 Hausa
 Indonesian
 Italian
 Japanese
 Javanese
 Malay
 Persian
 Portuguese
 Punjabi
 Russian
 Spanish
 Swahili
 Telugu
 Vietnamese