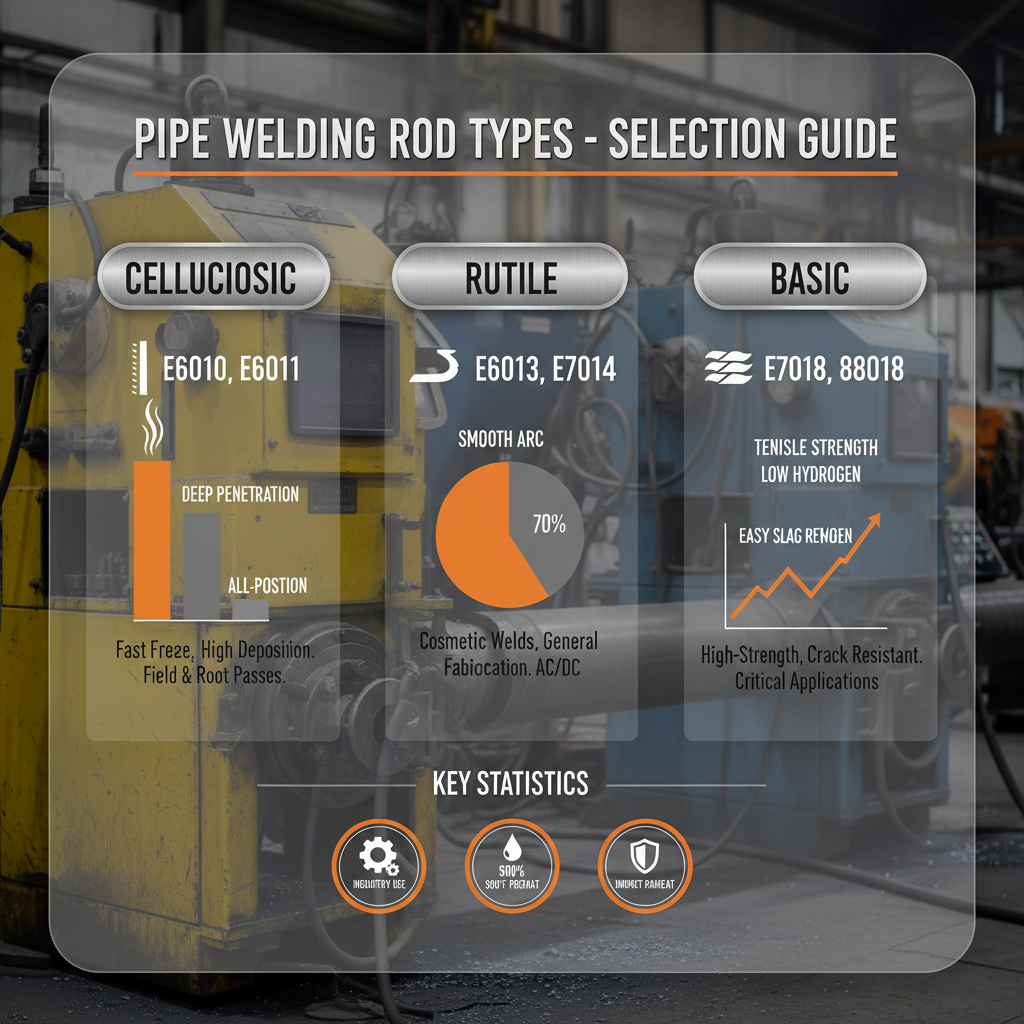
Selecting the correct welding consumable is one of the most critical decisions in any fabrication project, as the wrong choice can lead to structural failure or premature corrosion. A comprehensive welding rod cheat sheet serves as an essential guide for engineers and technicians to navigate the complex world of electrode classifications and material compatibility. By simplifying the relationship between base metals and filling materials, these guides ensure that every joint meets industry standards for strength and durability.
Across the global manufacturing landscape, the demand for precision in welding has increased alongside the adoption of high-performance alloys. Whether working with carbon steel, stainless steel, or cast iron, understanding the nuances of AWS (American Welding Society) classifications is paramount. A reliable welding rod cheat sheet transforms technical data into actionable knowledge, reducing costly errors and improving the overall efficiency of the welding process in heavy industrial environments.
For professionals managing complex projects in power plants or chemical facilities, utilizing a welding rod cheat sheet ensures that the specific properties of materials, such as chromium stainless steel, are properly addressed. This systematic approach to selection prevents common issues like weld cracking and oxidation, providing a roadmap for selecting the right coating and current for every specific application.
Understanding Stainless Steel Electrode Selection
Selecting the appropriate stainless steel electrode requires a deep understanding of the base metal's chemistry. Chromium stainless steels are prized for their heat resistance and wear resistance, making them indispensable in petroleum and chemical equipment. However, their poor weldability means that a welding rod cheat sheet must be used to carefully match the electrode to the specific grade of chromium content to avoid structural defects.
For instance, when dealing with CR-13 stainless steel, the risk of cracking is significantly higher due to increased hardness after welding. The selection process involves deciding between using a matching chromium stainless steel electrode, which requires strict thermal controls, or opting for a chromium-nickel stainless steel electrode if post-weld heat treatment is not feasible.
Material Compatibility and Corrosion Resistance
Corrosion resistance is a primary driver in the selection of welding consumables. Chromium stainless steels provide excellent defense against oxidizing acids, organic acids, and cavitation, which is why they are the standard for high-pressure environments in power plants. Ensuring the weld metal maintains these properties requires precise electrode matching.
In the case of Chromium 17 stainless steel, elements like Titanium (Ti), Niobium (Nb), and Molybdenum (Mo) are added to enhance stability and corrosion resistance. This makes these materials more weldable than their CR-13 counterparts, though they still require specific handling as outlined in a professional welding rod cheat sheet.
Chromium-nickel (CR-NI) electrodes are particularly valued for their superior oxidation resistance. These are widely utilized in the manufacturing of medical machinery and fertilizer plants, where chemical stability is non-negotiable for safety and longevity.
Thermal Management and Preheating Requirements
Thermal control is the most critical factor in preventing weld failure. When using matching chromium stainless steel electrodes (such as G202 or G207) for CR-13 steel, preheating the base metal above 300°C is mandatory to prevent cracking. This rigorous process is a key highlight in any technical welding rod cheat sheet.
For Chromium 17 stainless steel, the thermal requirements shift slightly, requiring preheating above 200°C and a tempering process around 800°C after welding. If the equipment's dimensions or location make heat treatment impossible, switching to a chromium-nickel electrode (A107 or A207) is the recommended solution.
Failure to adhere to these thermal protocols often results in immediate cracking or long-term fatigue. A welding rod cheat sheet provides the necessary temperature benchmarks to ensure that the transition between the heat-affected zone and the weld bead remains stable.
Coating Types and Power Supply Interaction
The chemistry of the electrode coating dictates both the weld quality and the power source required. Chromium-nickel stainless steel coatings generally fall into two categories: titanium-calcium type and low hydrogen type. Understanding the interaction between these coatings and the power supply is a core component of a welding rod cheat sheet.
Calcium titanate coatings are versatile enough for both AC and DC power. However, AC welding often results in shallower penetration and a higher tendency for the weld to "redden" or oxidize. For these reasons, DC power supplies are strongly preferred to maintain the integrity of the stainless steel's protective layer.
Comparison of Electrode Performance Metrics
Precision Storage and Drying Protocols
Electrode coatings are highly hygroscopic, meaning they absorb moisture from the air, which can lead to porosity and hydrogen-induced cracking in the weld. To prevent this, a strict drying regimen is essential. Titanium-calcium type electrodes should be dried at 150°C for one hour, while low hydrogen types require a higher temperature of 200°C to 250°C for one hour.
It is crucial to avoid repeated drying cycles, as this can cause the coating to crack and peel off from the core wire. Furthermore, operators must ensure that electrodes remain free of oil and dirt; any contamination can increase the carbon content of the weld, compromising the corrosion resistance of the stainless steel structure.
Current Optimization and Bead Control
Managing the welding current is vital to prevent intergranular corrosion. When welding stainless steel, the current should generally be about 20% lower than what would be used for a standard carbon steel electrode. This reduced heat input prevents the precipitation of carbides at the grain boundaries.
Arc length must be kept short to minimize the heat-affected zone. A technique emphasizing quick cooling between layers and the creation of narrow beads is recommended to ensure the material's properties remain intact.
Additionally, the positioning of the weld affects the choice of diameter. Electrodes with diameters of 3.0mm and below are suitable for all-position welding, whereas those above 3.0mm are restricted to flat and fillet welding applications.
Technical Specifications for AWS E308-16
The CB-A102 electrode, corresponding to AWS E308-16, is a specialized consumable designed for corrosion-resistant structures. It is specifically engineered for welding 0Cr19Ni9 and 0Cr19Ni11Ti stainless steels in environments where temperatures remain below 300°C.
This electrode utilizes a lime-titania coating and is optimized for DC power supplies. Its mechanical properties are impressive, boasting a tensile strength (Rm) of ≥550 Mpa and an elongation (A) of ≥35%, ensuring both strength and ductility in the finished joint.
The chemical composition of the deposited metal is strictly controlled, with Chromium levels between 18.0-21.0% and Nickel between 9.0-11.0%, providing the essential balance required for high-performance chemical and industrial applications.
Technical Analysis of AWS E308-16 Electrode Specifications
|
Property Dimension
|
Specification Value
|
Material Grade
|
Application Limit
|
| Tensile Strength |
≥550 Mpa |
AWS E308-16 |
Below 300°C |
| Elongation |
≥35% |
CB-A102 |
Corrosion-Resistant |
| Chromium Content |
18.0-21.0% |
0Cr19Ni9 |
Industrial Piping |
| Nickel Content |
9.0-11.0% |
0Cr19Ni11Ti |
Chemical Tanks |
| Coating Type |
Lime-Titania |
Stainless Steel |
All Positions (≤3mm) |
| Current Type |
DC Preferred |
AWS Standard |
High-Precision Joints |
FAQS
If post-weld heat treatment is not possible, you should avoid matching chromium stainless steel electrodes like G202 or G207. Instead, use a chromium-nickel stainless steel electrode, such as A107 or A207, which provides better weldability and reduces the risk of cracking without requiring extreme temperature cycles.
Stainless steel is more sensitive to heat. Using a current that is approximately 20% lower than carbon steel prevents overheating, which in turn avoids intergranular corrosion and minimizes the width of the heat-affected zone, preserving the material's corrosion-resistant properties.
Titanium-calcium type electrodes should be dried at 150°C for 1 hour. Low hydrogen types require a higher temperature of 200°C to 250°C for 1 hour. It is critical not to repeat the drying process, as this can lead to the coating cracking or peeling off.
Yes, but it depends on the diameter. Electrodes with a diameter of 3.0mm and below are suitable for all-position welding. For diameters above 3.0mm, the application is limited to flat and fillet welding to ensure proper bead formation and penetration.
While calcium titanate can be used with both, DC power provides deeper penetration and prevents the weld from becoming "red" (oxidizing) as easily as AC welding does, resulting in a cleaner, stronger weld with better metallurgical properties.
The addition of these stabilizing elements improves both the weldability and the corrosion resistance of Chromium 17 stainless steel, making it easier to weld compared to Chromium 13, although preheating at 200°C is still recommended.
Conclusion
Mastering the selection of welding consumables through a structured welding rod cheat sheet is the only way to ensure structural integrity in high-stakes industrial environments. From the precise thermal requirements of CR-13 stainless steel to the chemical balance of AWS E308-16 electrodes, every detail—including drying temperatures and current optimization—plays a pivotal role in preventing failure and maximizing corrosion resistance.
As manufacturing moves toward more advanced alloys and stricter safety standards, the reliance on accurate technical data becomes even more critical. By implementing rigorous electrode management and adhering to professional selection guides, fabricators can achieve superior weld quality that stands the test of time and extreme conditions. For professional-grade consumables and expert guidance, visit our website: www.jinlongweldingelectrode.com