

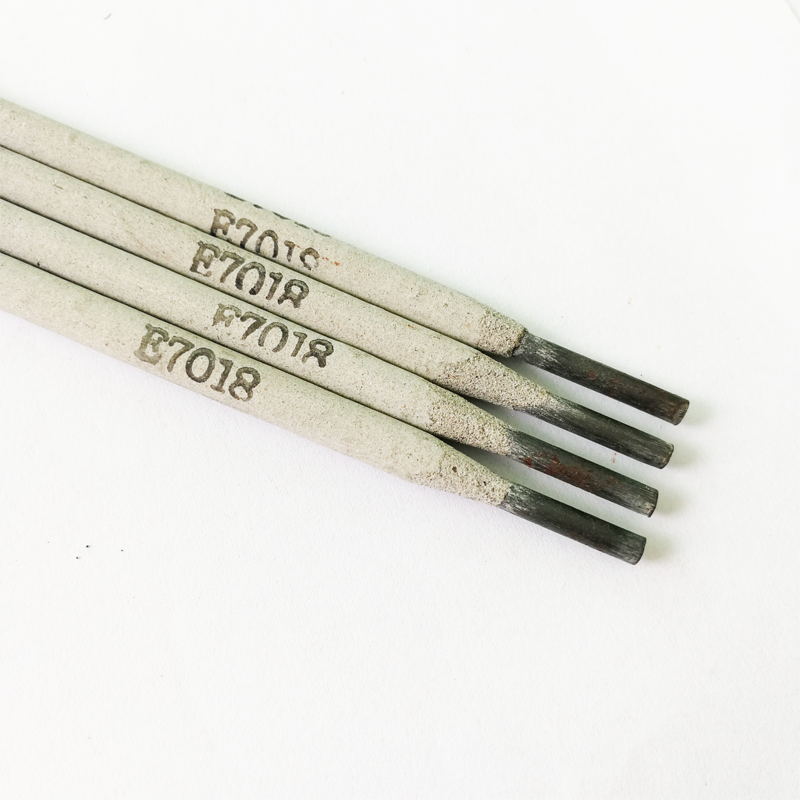
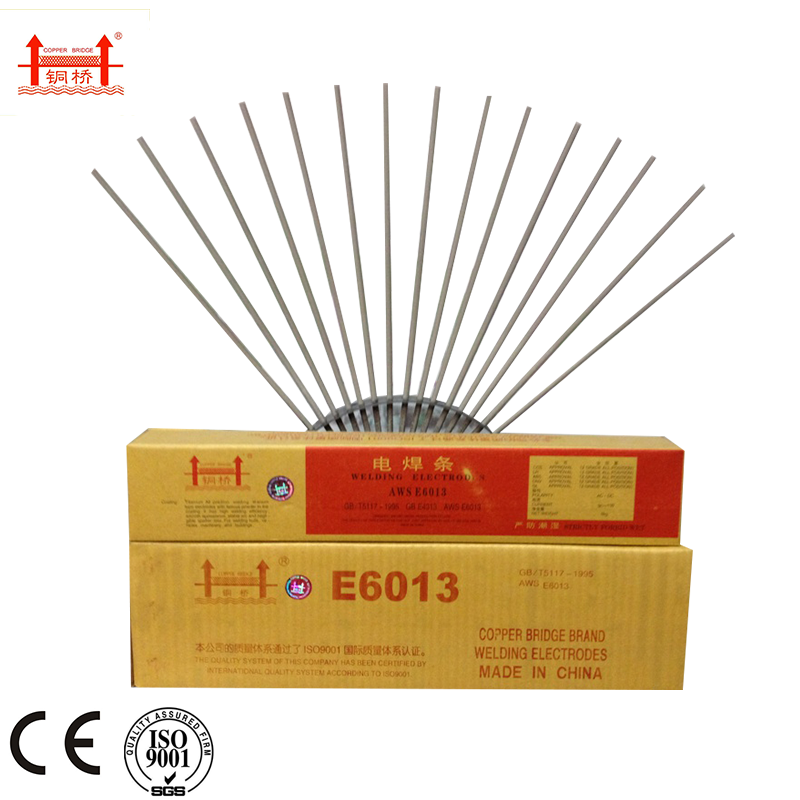
Copper Bridge E7018 Welding Rods China Factory Suppliers High Strength Low Hydrogen Electrodes



Related News
2026-07-01 09:32:39
Comprehensive Guide to Selection of Types of Welding Rods PDF
Selecting the correct filler metal is the cornerstone of any successful welding project. Whether you are working on heavy-duty carbon steel pipelines or intricate structural components, understanding the various types of welding rods pdf resources is essential for ensuring weld integrity and structural safety. The choice of electrode affects not only the strength of the joint but also the ease of penetration and the final appearance of the bead. In this comprehensive guide, we will explore the technical specifications of high-performance rods, such as the CB-J425, to help you optimize your manufacturing process.
2026-06-29 16:50:39
Comprehensive Guide to Types of Welding Rods and Uses PDF
Comprehensive Guide to Types of Welding Rods and Uses PDF Selecting the correct filler metal is the most critical step in ensuring the structural integrity and corrosion resistance of any welded joint. For professionals seeking a detailed types of welding rods and uses pdf , understanding the distinction between various alloys is essential. Whether you are working with chromium stainless steel for power plants or chromium-nickel variations for medical machinery, the choice of electrode directly impacts the welds longevity. In this guide, we analyze the technical specifications and industrial applications of high-performance welding electrodes to help you achieve precision and durability in every bead.
2026-06-27 15:42:52
Guide to Types of Welding Electrodes and Their Uses PDF Manual
Understanding Types of Welding Electrodes and Their Uses PDF Guide Selecting the correct filler metal is critical for the structural integrity and longevity of any welded joint. Whether you are working in power plants, chemical processing, or petroleum equipment, knowing the types of welding electrodes and their uses pdf documentation provides the necessary technical foundation to avoid common failures like cracking or corrosion. Chromium stainless steel and chromium-nickel alloys offer specialized resistance to oxidizing acids and high temperatures, but they require precise handling. This guide explores the technical specifications and application methods for high-performance electrodes to ensure professional-grade welding results.
2026-06-26 14:50:28
Expert Guide to the selection of electrode in welding for Success
Mastering the Selection of Electrode in Welding for Industrial Success Achieving a high-quality weld starts long before the arc is struck; it begins with the precise selection of electrode in welding . Whether you are working on heavy structural steel or delicate thin-plate components, the choice of electrode determines the mechanical strength, appearance, and longevity of the joint. Using the wrong filler material can lead to porosity, cracking, or insufficient penetration, compromising the safety of the entire structure. In this guide, we will explore the critical factors involved in choosing the right welding consumables to ensure professional-grade results in the manufacturing sector.
2026-06-25 16:48:22
Professional Guide on how to choose welding rod size for Steel
Mastering the Art of Welding: How to Choose Welding Rod Size Selecting the correct filler metal is one of the most critical decisions a welder makes to ensure the structural integrity and aesthetic quality of a joint. Understanding how to choose welding rod size can mean the difference between a professional-grade weld and a failure-prone joint. Whether you are working with mild steel, carbon steel, or low alloy steel, the diameter of your rod directly impacts heat input, penetration depth, and the overall efficiency of the process. In this guide, we will explore the technical factors that influence sizing
2026-06-23 05:10:11
Mastering Stainless Steel Welding with e308l 16 amps Guide
Mastering the E308L 16 Amps Setting for Perfect Stainless Steel Welding Achieving a high-quality weld on stainless steel requires a precise balance of material science and machine calibration. When utilizing e308l 16 amps , the welder must consider the relationship between current, heat input, and penetration. E308L is a low-carbon variant of the 308 stainless steel electrode, designed specifically to prevent carbide precipitation and ensure maximum corrosion resistance. In this guide, we will explore how managing the amperagespecifically focusing on the 16-amp range for thin gaugescan drastically improve the structural integrity and aesthetic finish of your industrial projects.
2026-06-21 05:05:43
Ultimate Guide to Choosing the Right 304 tig rod for Welding
In the world of precision welding, selecting the correct filler metal is the difference between a structural failure and a flawless finish. The 304 tig rod is one of the most widely used consumables in the industry, prized for its exceptional corrosion resistance and versatility. Whether you are working on food processing equipment, chemical containers, or architectural accents, understanding the nuances of ER308L the standard filler for 304 stainless is essential. This guide provides a professional deep dive into the specifications, applications, and best practices for using these rods to ensure high-quality, durable welds.
2026-06-20 05:10:16
Precision Welding Guide for SS Welding Rod 2.5 mm Electrode
Mastering Precision Welding with SS Welding Rod 2.5 mm In the world of high-precision fabrication, the choice of consumables can make or break the structural integrity of a project. The ss welding rod 2.5 mm is a cornerstone for professionals seeking a perfect balance between penetration and control. Whether you are working on intricate food-grade piping or heavy-duty industrial supports, selecting a rod with the correct diameter is essential for minimizing distortion and ensuring a clean, slag-free finish. This guide will explore the technical nuances, application methods, and comparative advantages of using a 2.5 mm stainless steel welding electrode to achieve industrial-grade results.

 English
 Arabic
 Bengali
 China
 French
 German
 Hausa
 Indonesian
 Italian
 Japanese
 Javanese
 Malay
 Persian
 Portuguese
 Punjabi
 Russian
 Spanish
 Swahili
 Telugu
 Vietnamese